

Uncategorized
Stone Polishing Machine: Types, Applications, Process, and Selection Guide
9月
A consistent stone finish depends on more than the polishing stage alone. The stone material, starting surface condition, abrasive progression, machine configuration, tooling, water management, and required finish all affect the final result. For fabricators, choosing the right stone polishing machine means looking at the complete processing workflow rather than the polishing head by itself.
Different workpieces also require different approaches. A large granite slab may need a continuous polishing line, while a tombstone, column, cylindrical workpiece, or special-shaped stone may require a more flexible machine configuration.
This guide explains how stone polishing works, the main types of polishing machines, suitable stone materials, abrasive selection, common applications, and the factors to consider when selecting equipment.
What Is a Stone Polishing Machine?
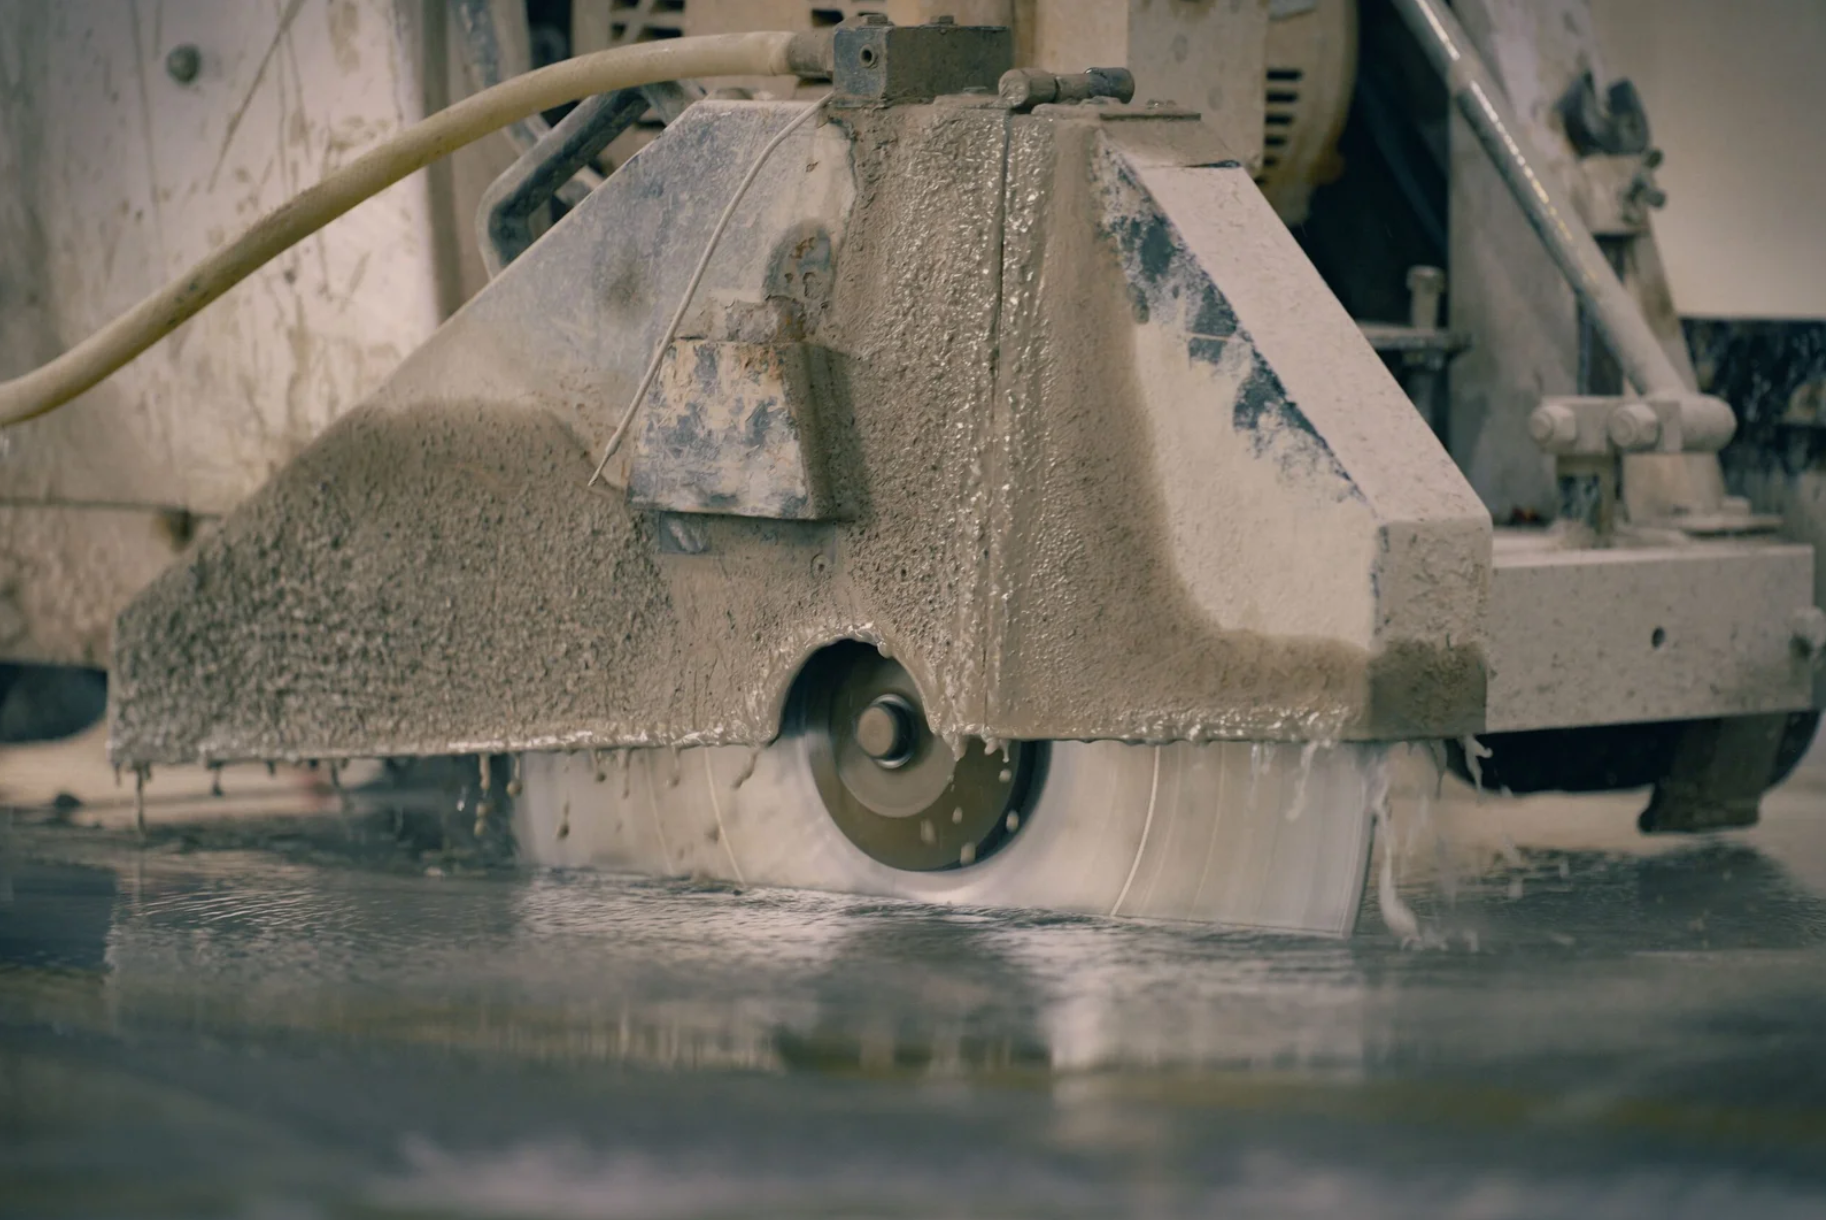
A stone polishing machine is equipment designed to refine and finish the surface of natural or engineered stone through controlled abrasive processing.
Depending on the machine configuration, the process may include grinding, honing, and final polishing. These stages gradually remove surface irregularities and scratches while producing the required surface appearance.
The terminology used in stone processing can vary between applications and regions. The Natural Stone Institute Glossary of Stone Industry Terms provides industry terminology covering a wide range of stone fabrication and finishing terms.
In practical production, polishing should not be viewed as an isolated operation. The final finish depends heavily on what happens before the polishing stage.
How Does a Stone Polishing Machine Work?
A typical stone polishing process follows a progression from heavier material removal to increasingly fine surface refinement.
Surface Preparation
Before polishing begins, the stone surface must be brought into a suitable condition.
Saw marks, uneven areas, tool marks, resin treatment, surface variations, and other imperfections can affect the later polishing stages. If the starting surface is inconsistent, the polishing process may produce uneven gloss or visible defects.
For this reason, surface preparation often determines how efficiently the following grinding and polishing stages can work.
Grinding
Grinding removes more material than the later finishing stages. It can level the surface, reduce saw marks, and remove deeper irregularities.
The abrasive used at this stage is generally coarser than the abrasives used for honing or polishing. The exact abrasive sequence depends on the stone material, initial surface condition, equipment, and desired finish.
For manufacturers handling different types of stone, equipment flexibility becomes important. CANON Machinery provides stone grinding and polishing machines for applications where surface preparation and finishing need to work together as part of a complete process.
Fine Grinding and Honing
After the main surface irregularities have been removed, finer abrasives refine the scratches left by the previous stage.
Honing generally produces a smoother, more uniform surface without the high reflectivity associated with a polished finish. The stage can also prepare the stone for the final polishing operation.
The transition from grinding to honing should be controlled rather than treated as a simple change of abrasive. Each stage needs to remove the surface marks generated by the previous stage.
Final Polishing
Final polishing uses finer abrasive tools to further refine the stone surface and develop the required appearance.
For polished stone, the objective is usually a smooth, reflective surface. However, the exact finish depends on the stone itself, tooling, abrasive progression, machine stability, and processing conditions.
A polishing machine therefore needs to maintain consistent contact between the abrasive and the workpiece while allowing the operator or control system to manage the processing sequence.
Types of Stone Polishing Machines
Stone polishing machines can be categorized according to their level of automation, flexibility, and processing configuration.
Manual Stone Polishing Machines
Manual machines give operators greater control over individual workpieces. They can be useful for smaller production volumes, custom work, repairs, and applications where stone dimensions or shapes vary frequently.
Their flexibility can be useful when a standardized automated line would not be practical.
However, results depend more heavily on operator technique and consistent process control.
Semi-Automatic Stone Polishing Machines
Semi-automatic equipment combines mechanical processing with operator intervention.
These machines can provide more consistent movement and pressure control than fully manual processing while still allowing operators to adjust the process for different materials or workpiece conditions.
They can be suitable for fabricators that need greater repeatability without committing to a fully automated production line.
Automatic Stone Polishing Machines
Automatic machines reduce manual intervention and can provide more consistent processing across repeated workpieces.
They are particularly useful when production involves standardized stone dimensions, repeatable surface requirements, or continuous slab processing.
Automation can also help integrate polishing with other production stages, material handling, drying, or quality-control procedures.
A Stone World fabrication case study describes an automated granite slab process in which slabs moved through preparation, treatment, drying, and polishing stages as part of an integrated production workflow. The example illustrates how polishing can form one stage within a larger automated fabrication system. Read the Stone World fabrication case study on automated granite slab enhancement.
CNC Stone Polishing Machines
CNC equipment uses programmed movement to process workpieces with more complex geometries.
This configuration can be useful for shaped stone components, architectural elements, custom profiles, and other applications where tool movement needs to follow defined geometries.
The advantage is not simply automation. CNC control can also make repeatable processing of complex shapes more practical.
Multi-Head Stone Polishing Machines
Multi-head machines use multiple processing heads to progressively work across the stone surface.
This configuration is common in continuous slab processing and other applications where several abrasive stages need to be completed in sequence.
The number and arrangement of heads should match the intended process rather than being selected independently from the stone material and required finish.
What Types of Stone Can a Stone Polishing Machine Process?
The appropriate polishing process varies significantly between stone materials.
Granite
Granite is hard and abrasive, so it typically requires a controlled grinding and polishing sequence.
The starting condition of the slab also matters. Saw marks, surface variation, resin treatment, and natural mineral differences can affect abrasive selection and polishing behavior.
Marble
Marble is generally softer than granite and can respond differently to abrasive processing.
Excessive material removal is not always necessary, so the process should focus on controlled surface refinement and scratch removal. The required finish also influences the final abrasive stages.
Quartzite
Natural quartzite should not simply be treated as another form of quartz.
Its mineral composition and hardness can make grinding and polishing more demanding than some other stone materials. Tool selection and process conditions should therefore be developed around the specific material rather than a generic stone-polishing sequence.
Engineered Quartz and Sintered Materials
Engineered quartz and sintered materials are manufactured products with different compositions and surface structures from natural stone.
Their processing behavior can vary between products and manufacturers. Abrasive compatibility, tooling recommendations, cooling requirements, and the desired finish should be considered before establishing a production sequence.
For these materials, following the material supplier’s processing guidance can help avoid unnecessary tool wear or surface defects.
Applications of Stone Polishing Machines
A stone polishing machine may be used in several areas of stone fabrication.
Stone Slabs
Slab processing is one of the most common applications.
The process may include surface grinding, honing, polishing, buffing, drying, and inspection. Continuous production lines are often designed around the dimensions and production requirements of the slabs being processed.
Tombstones and Monuments
Tombstones and monuments may require grinding and polishing across flat surfaces as well as shaped or decorative sections.
The required machine configuration depends on the workpiece dimensions, geometry, finish, and production volume.
Cylindrical Stone
Cylindrical stone components require a different processing approach from flat slabs.
The machine needs to maintain suitable contact with the curved surface while controlling abrasive movement and finishing consistency.
Columns
Stone columns may combine cylindrical, tapered, or decorative geometries.
In these applications, profiling and surface finishing often need to work together. The geometry should be established before the final polishing stages.
Prisms and Stone Lines
Prismatic components and stone lines may require controlled shaping followed by grinding and finishing.
The required process depends on the cross-section, dimensions, material, and final surface specification.
Special-Shaped Stone
Special-shaped stone products can include custom architectural components, decorative elements, and irregular geometries.
These applications often benefit from flexible or CNC-controlled equipment because the workpiece geometry cannot be treated like a standard flat slab.
Grinding vs. Honing vs. Polishing
Although these terms are sometimes used interchangeably, they describe different stages of surface finishing.
Process Main Purpose Typical Result
Grinding Remove material, saw marks, and deeper irregularities Prepared and leveled surface
Honing Refine scratches and surface roughness Smooth matte or satin finish
Polishing Further refine the surface Glossy or reflective finish
The stages are connected. A polishing operation cannot always compensate for poor grinding or incomplete honing.
If deeper scratches remain after grinding, moving directly to a very fine polishing stage may waste abrasive material and increase processing time without producing a consistent finish.
Abrasives Used for Stone Polishing
Abrasives are central to the stone finishing process.
Common abrasive systems may include diamond tools, abrasive blocks, polishing pads, and other finishing compounds or tools designed for specific materials.
The abrasive choice depends on:
Stone type
Stone hardness
Starting surface condition
Required finish
Machine configuration
Tool compatibility
Production requirements
There is no single universal grit sequence that works for every stone and machine.
A fabricator should instead establish an abrasive progression that allows each stage to remove the marks produced by the previous stage.
Why Abrasive Progression Matters
Abrasive progression is one of the most important parts of consistent stone polishing.
A typical process moves from relatively aggressive material removal toward progressively finer surface refinement.
For example:
Surface preparation → coarse grinding → finer grinding → honing → polishing → final inspection
The exact sequence can change according to the material and finish.
If an abrasive stage is too aggressive, it may create unnecessary scratches that require additional processing. If the abrasive is too fine for the starting surface, it may not remove the previous scratches efficiently.
The objective is not simply to use more abrasive stages. It is to create a logical progression in which every stage prepares the surface for the next one.
The Role of Water in Stone Polishing
Water plays an important role in many stone grinding and polishing processes.
It can help control heat generated during abrasive contact, assist with lubrication, and remove stone slurry from the working area.
Poor water management can affect polishing consistency. Excessive slurry accumulation may interfere with abrasive contact, while inadequate cooling can affect tooling and surface conditions.
For production equipment, water supply, drainage, slurry removal, and machine cleanliness should therefore be considered part of the processing system.
Factors That Affect Polishing Quality
A consistent polished finish depends on several variables working together.
Stone Material
Different stones have different hardness, mineral composition, porosity, and surface behavior.
The same abrasive progression may therefore produce different results on granite, marble, quartzite, and engineered materials.
Initial Surface Condition
A surface with deeper saw marks or uneven areas requires more preparation before final polishing.
Starting with a more consistent surface can reduce the workload of later stages.
Abrasive Selection
The abrasive must match the material and the processing stage.
Using an unsuitable abrasive can lead to slow material removal, excessive tool wear, scratches, or inconsistent gloss.
Machine Stability
Consistent mechanical movement helps maintain uniform abrasive contact.
Machine rigidity, head movement, workpiece support, and process control can all influence surface consistency.
Tool Condition
Abrasives gradually wear during production.
A worn tool may change the cutting behavior and affect the surface finish. Regular inspection and timely replacement help maintain a more stable process.
Water and Slurry Management
Cooling and slurry removal influence both tooling and surface quality.
Water flow should be appropriate for the equipment and process rather than treated as a secondary consideration.
How to Choose a Stone Polishing Machine
Choosing a stone polishing machine should start with the workpiece and production process rather than the machine name alone.
1. Identify the Stone Materials
List the materials that will be processed.
If the factory handles several types of stone, consider whether the equipment can accommodate different abrasive systems and processing conditions.
2. Define the Workpiece Geometry
Flat slabs, tombstones, cylindrical stone, columns, and special-shaped components may require very different machine configurations.
Geometry should therefore be one of the first selection criteria.
3. Define the Required Finish
Determine whether the product requires:
Ground finish
Honed finish
Satin finish
Polished finish
High-reflectivity finish
A combination of surface finishes
The required result affects the abrasive progression and machine configuration.
4. Consider Production Volume
Manual equipment may make sense for variable, lower-volume work, while automated systems can be more appropriate for repetitive production.
The key is to match the automation level to the actual workflow.
5. Evaluate the Complete Process
A polishing machine should not be evaluated separately from grinding, profiling, handling, drying, water management, and inspection.
For shaped stone products, profiling may need to happen before grinding and polishing. CANON Machinery also offers stone profiling machines for applications where shaping and surface finishing are connected.
6. Consider Maintenance and Serviceability
A machine should be practical to operate and maintain.
Important considerations include access to working components, abrasive replacement, water management, routine cleaning, machine adjustment, and availability of technical support.
Common Stone Polishing Problems
Several problems can appear when the processing sequence or machine conditions are not properly matched.
Uneven Scratches
Uneven scratches may result from incomplete previous-stage processing, inconsistent abrasive contact, unsuitable abrasive progression, or worn tooling.
The solution is usually to identify which stage introduced the problem rather than simply increasing the final polishing time.
Uneven Gloss
Different levels of gloss across the same surface can result from inconsistent material conditions, tool wear, machine movement, water management, or insufficient processing at earlier stages.
Dull Finish
A dull surface may indicate that the final abrasive stage is not properly matched to the stone or that previous scratches remain.
Surface cleanliness and tooling condition should also be checked.
Excessive Tool Wear
Rapid tool wear may occur when abrasive selection does not match the material, when processing conditions are unsuitable, or when the tool is working against an unnecessarily difficult surface condition.
Stone Polishing vs. Stone Profiling
Stone polishing and stone profiling solve different problems.
Profiling focuses on creating or refining the geometry of the stone.
Grinding focuses on removing material and preparing the surface.
Polishing focuses on refining the surface appearance.
A shaped stone product may therefore follow a sequence such as:
Profiling → Grinding → Honing → Polishing → Inspection
For a flat slab, the workflow may be much simpler:
Grinding → Honing → Polishing → Inspection
The exact sequence depends on the product geometry and finish requirements.
Typical Stone Processing Workflow
Workpiece Typical Processing Approach
Stone slabs Grinding → Honing → Polishing
Tombstones Shaping → Grinding → Polishing
Cylindrical stone Profiling → Grinding → Polishing
Columns Shaping → Profiling → Polishing
Prismatic stone Profiling → Finishing
Stone lines Shaping → Grinding → Finishing
Special-shaped stone Profiling → Surface finishing
These are general process relationships rather than fixed production recipes. Actual abrasive sequences and machine configurations should be adjusted according to the stone material, workpiece geometry, and required finish.
How to Build a Consistent Stone Polishing Workflow
A consistent process starts with the stone rather than the machine.
First, inspect the incoming material and identify its surface condition. Determine whether the stone has deep saw marks, uneven areas, resin treatment, or other characteristics that could affect grinding.
Next, establish the required final finish and work backward through the abrasive stages.
Each stage should remove the surface marks created by the previous stage. Avoid moving to a very fine abrasive before the surface is adequately prepared.
Tool condition should also be monitored throughout production. A polishing process can become inconsistent when worn abrasives remain in service for too long.
Water and slurry management should remain stable across production. Changes in cooling or slurry removal can affect both tooling behavior and surface quality.
Finally, inspect the stone between major processing stages. Early detection of scratches, unevenness, or other defects is easier to correct than defects discovered after final polishing.
Final Thoughts
A stone polishing machine is only one part of a complete stone processing system.
The final surface depends on the relationship between the stone material, initial surface condition, grinding, abrasive progression, polishing, machine configuration, tooling, water management, and final inspection.
For manufacturers, the most useful approach is to define the complete workflow first and then select equipment around that workflow. Flat slabs, tombstones, columns, cylindrical stone, and special-shaped products may all require different combinations of profiling, grinding, honing, and polishing.
A well-matched process can make surface finishing more consistent and easier to control while allowing equipment to fit the actual production requirements of the stone fabrication operation.
